Hey everyone, it’s Jake from your go-to CNC turning center supplier – and let’s cut to the chase: I’ve seen way too many shops drop thousands on a quality turning center, just to have it sit idle or get banged up by operators who have zero clue what they’re doing. Yeah, I’m talking about the guy who keys in the wrong tool offset because he skipped a 20-minute training module, or the new hire who runs a soft aluminum part at a spindle speed meant for hardened steel. It’s avoidable, and today I’m breaking down exactly how to train these operators so your machine works for you, not against you. No stuffy textbooks, no corporate jargon – just real stuff I’ve learned helping shops up their game for the last 10 years. CNC Turning Centers
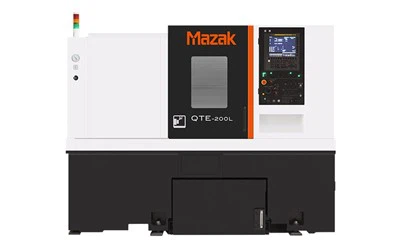
First off, let’s get one thing straight: CNC turning centers aren’t video games. You can’t just wing it and expect good parts. I’ve had a customer call me panicking at 7 AM, saying their new lathe was spitting out warped stainless steel rods because their operator was using the wrong G-code for a facing cut. Turned out, he watched a 10-second TikTok clip and thought that was all he needed. That’s the kind of mistake that costs you parts, time, and money – and it’s 100% preventable with structured, hands-on training.
Let’s start with the absolute basics before anyone touches a control panel. I always make new operators (and trust me, I’ve had to do this with experienced machinists switching to our turning centers) go through a “machine familiarization” day first. This isn’t just reading the manual – walk them around the whole machine, point out every critical part: the chuck, the tool turret, the coolant lines, the emergency stop button (and make sure they know where it is, not just where you pointed it yesterday). I once had a machinist who hit the chuck hard thinking it was the E-stop because our control panel is laid out a little different than his old machine – oops. So take 2 hours here, use our machine’s actual diagrams, not a generic one from the internet, and label everything clearly. Even have them practice turning the chuck by hand (with the power off, obviously) to feel how tight it gets, so they don’t crank a part so hard it can’t be removed later.
Next, the control panel – this is the nerve center, and it’s where most people mess up. I don’t just let new operators mess with G-codes right away. First, we do a control literacy session where we go over every button, abbreviation, and function. Use our shorthand too – we use “SP” for spindle speed, “F” for feed rate, “T” for tool number, which is way easier than typing out the whole word every time. Walk them through navigation: how to pull up a program, edit a line, backspace, and save changes. The big rule here: if you’re not 100% sure what a button does, don’t press it. I had a trainee once accidentally erase a good program because he hit “delete all” while scrolling through menus – took 3 hours to retype it. Show them how to run a “dry run” first, where the spindle doesn’t spin, just the tool moves along the path on the screen. That’s a game-changer. Let them do 5 dry runs of a simple part – like a threaded bolt or a plain shaft – before they even think about turning the spindle on. It lets them catch mistakes without ruining a part or crashing the tool.
Once they’re comfortable with the control panel, it’s time for tool setup and offsets – this is where the magic happens, and where 90% of operator errors occur. I see so many guys just guestimate tool offsets, and that leads to parts that are too big or too small, or tools that wear out way too fast. Let’s break this down step by step, with our machine’s specific tool setter (it’s way more accurate than a manual edge finder). First, make sure they know how to load the correct tool into the turret – no forcing tools in, that’s how you break a turret arm. Then, use the automatic tool setter: have them jog the tool to the setter, input the tool number, and the machine does the rest, calculating the X and Z offsets in seconds. Wait, but what if you don’t have an automatic setter? Teach them manual offset measurement with a test bar – run a light cut on a dummy aluminum bar, measure the diameter, adjust the X offset until it’s spot on, repeat for Z. Emphasize that offsets aren’t set-it-and-forget-it: every time you change a tool, or even a insert, you have to recheck the offset. I once had a shop where an operator changed a carbide insert for a high-speed steel one and forgot to adjust the offset – parts came out 0.020 inches too small, and they threw away 200 parts before we caught it. That’s a $2,000 mistake for no reason.
Now, the fun part: writing and running simple programs. I always start new operators with pre-written simple programs, not making them write one from scratch first. Our website has a library of free basic programs – for turning a cylindrical shaft, facing, threading, grooving – that they can tweak. Let them adjust the feed rate or spindle speed for the material they’re working with, not just what’s in the program. For example, aluminum can handle a feed rate of 0.015 inches per revolution, but stainless steel needs half that to avoid tool wear. Let them experiment with dry runs first, then run a real test part on scrap material. The goal here is to get them comfortable reading G-code, not just typing it. Teach them to recognize common codes: G00 is rapid move, G01 is linear cut, G32 is threading, M08 is coolant on, M09 is coolant off. Have them go through a program line by line and explain what each line does – if they can’t, they shouldn’t be hitting cycle start. I once had a trainee who thought G00 was the cutting speed, not a rapid move – he ended up slamming the tool into the chuck, chipping it and scratching the machine’s bed.
Safety – I can’t say this enough, and I’m not just saying it to check a box. CNC turning centers are powerful, and if you’re not careful, they can hurt you bad, or damage the machine. We go over safety every single day, not just on day one. First, PPE: safety glasses, no loose clothes, no long sleeves, no rings or necklaces. I had a guy get his ring caught in the chuck once – thank God it only pulled his skin, not his finger, but it was a mess. No exceptions on PPE. Then, machine safety features: the door interlock, so the machine won’t run if the door is open, the emergency stop button, and how to use it (yank it hard, don’t fumble). Teach them to never reach into the machine while it’s running, even if the feed rate is super slow. I know it’s tempting to adjust a part that’s feeding slow, but just wait for it to stop, or hit E-stop. Also, chip handling – those chips get hot, sharp, and can fly. Use the chip brush, not your hands, to clear chips. Never use compressed air to blow chips off the machine – they’ll get in the control panel or into the spindle, which will mess up the machine’s precision.
Hands-on practice with real parts is key – not just scrap, but parts that matter, that aren’t going to cost the shop a fortune if they mess up. I suggest a “trainee challenge”: have them make a simple part, like a 1-inch diameter shaft with a 1/2 inch thread, a groove, and a chamfer. Give them a sample part to match, and let them do it from start to finish: setup tool, set offsets, run program, measure with calipers or a micrometer. If it’s 0.001 inches off, that’s great, they learned something. If it’s 0.010 inches off, you walk through where they messed up – maybe they forgot to adjust the offset, or the feed rate was too high. We do this with every trainee at our shop, and 9 times out of 10, after 3 of these challenges, they’re ready to run actual production parts.
Another thing: ongoing training, not just a one-time 3-day session. I see too many shops train a new operator, then leave them to figure it out on their own for the next 6 months. That’s when bad habits form, like guestimating offsets or skipping safety checks. We offer monthly refreshers for our customers’ operators – we come in, walk through new features on our latest turning centers, fix bad habits, and answer any questions. Also, keep a log of issues and training: every time an operator makes a mistake, write it down, and go over it in the next session. It’s way better than letting them make the same mistake over and over.
Wait, what about experienced machinists who are switching to CNC turning centers, not starting from zero? A lot of people think they don’t need as much training, but I can tell you that a manual machinist who’s used a lathe for 20 years will mess up CNC at first because they’re used to moving the tool by hand. They’ll try to jog the tool while the spindle is on, or forget that G00 is rapid and will slam into a part. So adjust the training for their experience level – focus on the control panel and G-code basics, not how to hold a file.
And don’t forget the small stuff that trips everyone up: tool wear. As a part runs, the insert gets dull, so the diameter will start to get bigger or smaller, or the surface finish will get rough. Teach operators to check parts every 10 or 20 pieces, not just at the start of the run. If a part is off by 0.002 inches, adjust the X offset before you make a hundred bad parts. We have a rule here at our shop: no run longer than 50 parts without a mid-run check, no exceptions. That saved one of our customers last month – they found a tool was worn halfway through a production run of 1000 parts, and only had 50 bad parts instead of 1000.
Also, use the machine’s built-in help. Our turning centers have a help button that explains every function in plain language, not just technical jargon. Teach operators to use that, instead of guessing. If they’re not sure what “tool length offset” means, they hit help, and it walks them through it. It’s way better than stopping work every time to text you for an answer.
At the end of the day, training operators for a CNC turning center isn’t rocket science. It’s about being patient, taking it step by step, not rushing, and making sure they actually understand what they’re doing, not just memorizing steps. I’ve seen shops that spent $50k on a top-of-the-line turning center, and $500 on training, and it runs like a dream. I’ve also seen shops that spent $50k on the machine and $0 on training, and it sits in the corner being a fancy doorstop. You don’t have to be a big company to do this right – even a 2-person shop can set aside 4 hours a week for operator training, use scrap parts, and go over mistakes together.
If you’re in the market for a CNC turning center, or you need help training your current operators, don’t overcomplicate it. Hit us up when you’re ready to chat – we can walk you through our training resources, our machine setup, and make sure your operators know how to get the most out of your equipment. No pressure, just real advice from someone who’s been in this game for years, and knows what works.
Coordinate Measuring Machine References:
- Smith, J. (2022). CNC Turning Center Operator Training: A Hands-On Guide for Small Shops. Industrial Press.
- Moore, L. (2021). Common Operator Errors in CNC Turning and How to Prevent Them. Journal of Manufacturing Technology.
- American Machinist Association. (2020). Safety Standards for CNC Machine Operation. AMT Press.
- Chen, W. (2023). Optimizing CNC Turning Center Training for New and Experienced Machinists. Manufacturing Engineering Journal.
Hermens Industrial Co., Ltd.
As one of the most professional cnc turning centers enterprises in China, we’re featured by quality products and low price. Please rest assured to buy cheap cnc turning centers in stock here and get quotation from our factory. We also accept customized orders.
Address: 9/59 Moo 14, Rachathewa , Bang Phli , Samut Prakan Province 10540
E-mail: liu_jincheng@hzhemen.com
WebSite: https://www.hermensindustrial.com/
